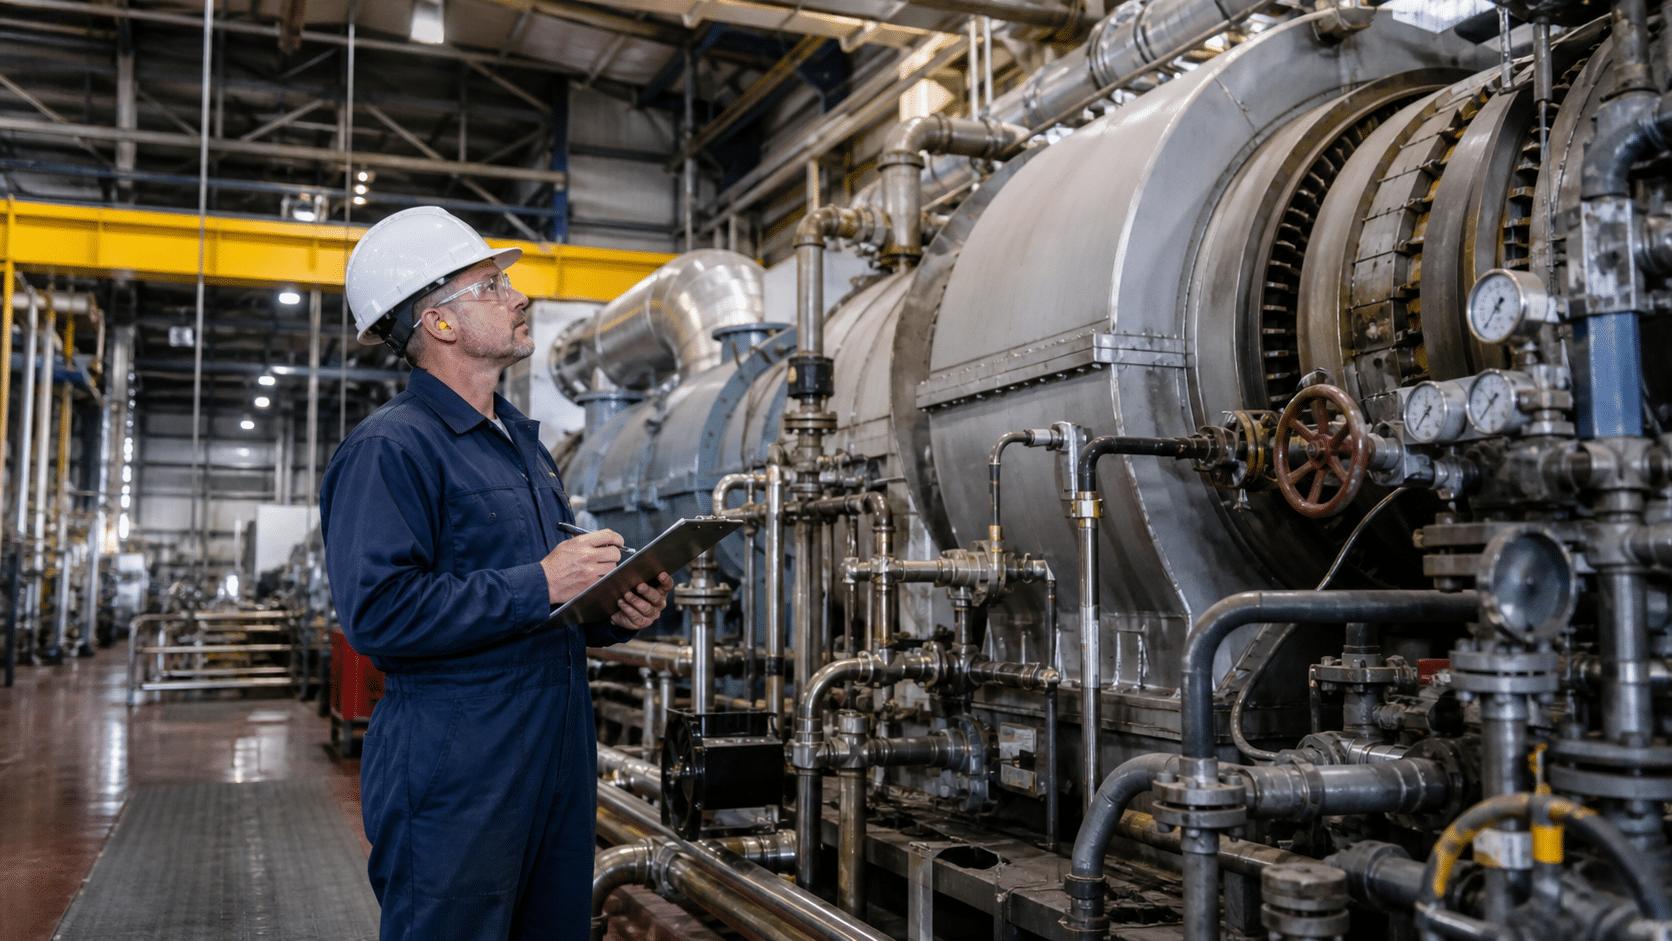
A chemical plant operator controls a process that turns raw materials into a product. The work may involve pumps, tanks, reactors, heat exchangers, control screens, samples, valves, and written procedures. Operators watch trends, make approved adjustments, and respond when the process moves outside normal conditions. The job requires technical focus, safety discipline, and comfort with shift work.
What does a chemical plant operator do?
The work differs by product and plant, but the operator usually connects control-room information with field conditions.
| Area | Typical work |
|---|---|
| Monitoring | Read instruments, alarms, charts, and process screens |
| Field rounds | Check pumps, valves, tanks, lines, leaks, noise, and heat |
| Process control | Adjust flow, pressure, temperature, level, or chemical feed |
| Sampling | Collect or test material and compare it with specifications |
| Startup and shutdown | Follow detailed procedures and communicate each step |
| Documentation | Record readings, changes, maintenance needs, and incidents |
Some operators work mainly from a control room. Others spend much of the shift in the unit. Either way, the job requires attention, teamwork, and respect for procedures. A small change in pressure or temperature can matter.
How do you become a chemical plant operator?
The closest BLS occupation, chemical plant and system operators, generally requires a high school diploma or equivalent and moderate-term on-the-job training. Employers may prefer experience in manufacturing, process operations, instrumentation, maintenance, or the military. Technical certificates in process technology, industrial systems, or chemistry can help, but the plant’s own training remains essential.
Experience as a process technician, instrumentation technician, or maintenance worker may transfer. It does not replace site qualification: each facility has its own equipment, hazards, products, and operating rules.
What are the safety requirements?
Chemical plants can expose workers to hazardous substances, pressure, heat, moving equipment, noise, and confined spaces. Training may cover hazard communication, respiratory protection, process safety, emergency response, lockout/tagout, and permit systems. Read the job’s physical and medical requirements carefully.
Operators should know when to stop and escalate a problem. Good documentation is part of safe operation because the next shift needs an accurate picture of what changed.
Chemical plant operator pay and outlook
The BLS lists chemical plant and system operators among occupations not covered in a full Occupational Outlook Handbook profile. Its 2025 benchmark is a median annual wage of $78,120, about 16,700 jobs, and projected 5% decline from 2025 to 2035. These figures are a benchmark for the occupation, not a promise for every job using the title.
Pay depends on the product, region, union status, shift premiums, overtime, and the level of process responsibility. A trainee offer can be well below a fully qualified operator’s wage.
Is it a good second career after 40?
It may fit someone who likes equipment, clear procedures, and work where small observations matter. Previous experience in manufacturing, utilities, water treatment, aviation, maintenance, or quality can provide useful examples. The rotating schedule and chemical environment deserve equal attention to the pay number.
Before applying, ask about shift rotation, training pay, background checks, protective equipment, and the path to qualification. A plant that runs continuously may require nights, weekends, holidays, and overtime.
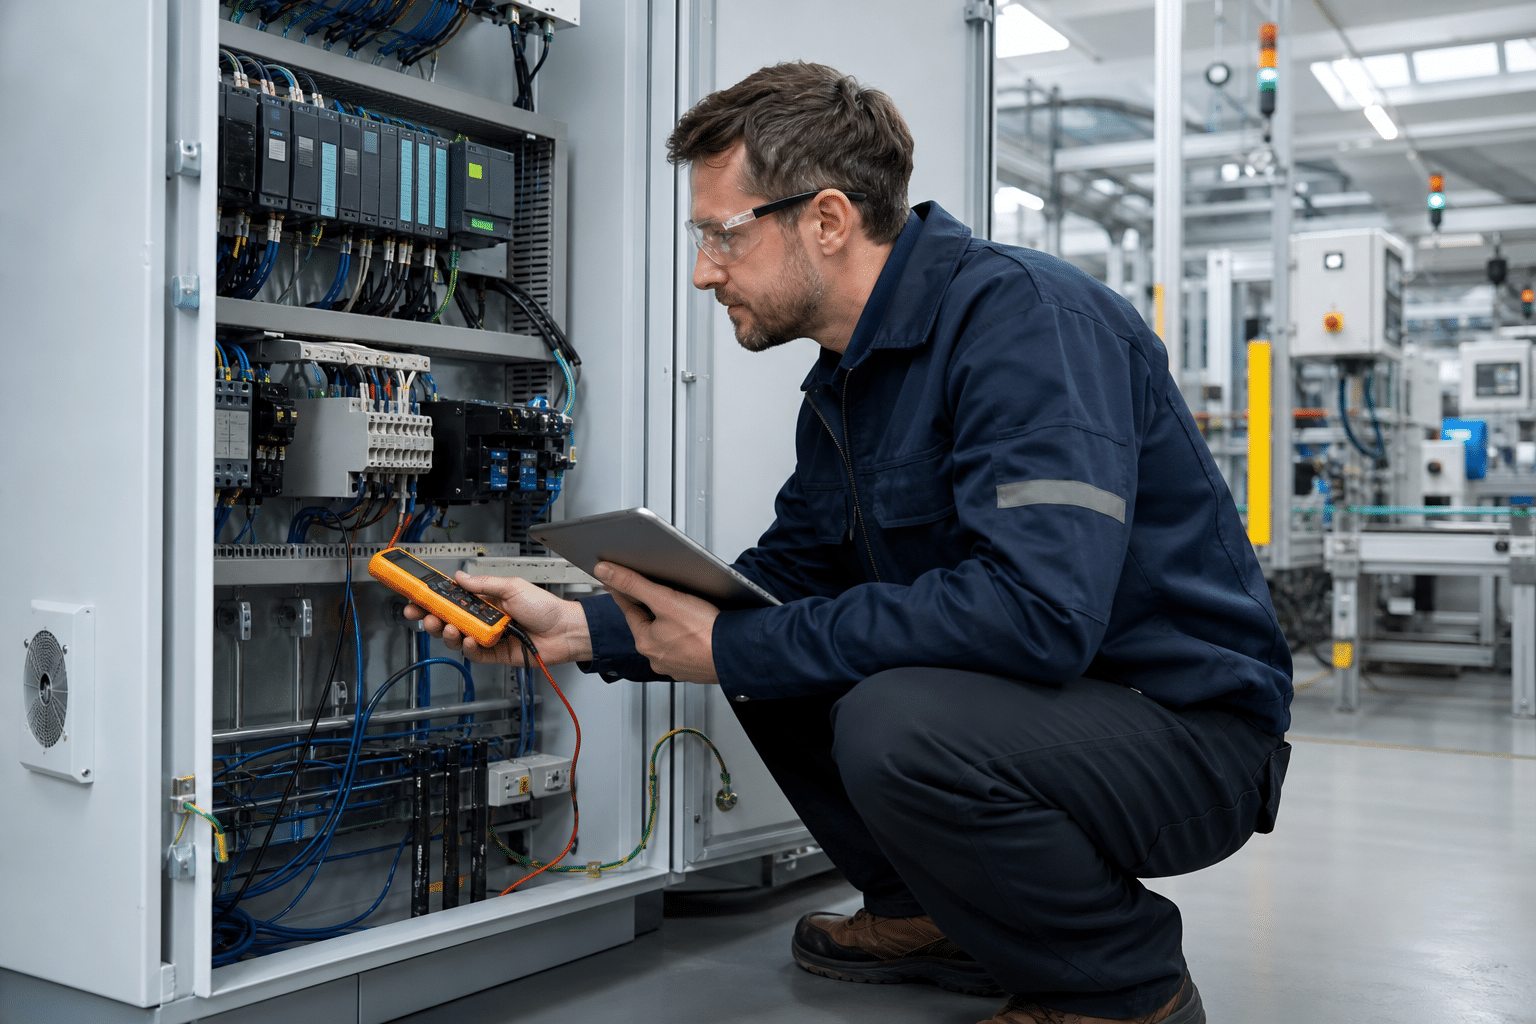
Process behavior matters more than one gauge: A temperature change may be linked to flow, pressure, a valve position, cooling, feed quality, or an instrument problem. The operator checks the trend and field condition, follows the response procedure, communicates with the team, and records what happened before making a larger adjustment.
Bottom line
Chemical plant operators keep a complex process within its operating limits. The work can be a realistic technical career change without an engineering degree, but training, safety, and shift demands are substantial. Compare the actual unit and employer before deciding whether the title fits you.
Related guides: Drafting Technician: Duties, Training, Pay and Career Fit and CNC Programmer: Duties, Training, Pay and Career Fit.
Learn the process as connected equipment
A chemical plant is easier to understand when you trace material and energy through the system. Follow what enters a vessel, what leaves it, which pumps move it, how temperature or pressure is controlled, and where relief or shutdown protection acts. Memorizing isolated limits is not enough. Operators need to recognize how one adjustment can change conditions downstream.
During training, compare the piping and instrumentation diagram with the field. Identify valves, instruments, sample points, drains, vents, and equipment numbers. Plants change over time, so report differences instead of assuming the drawing or label is correct. Never operate an unfamiliar valve simply because it appears to be in the expected location.
Make shift handovers useful
A good handover explains what changed, what remains abnormal, which permits or equipment isolations are active, and what the incoming operator must watch. Include exact times and trends when they matter. Saying a pump has been acting strange is far less useful than recording the noise, vibration, discharge pressure, operating mode, and when the condition began.
Control-room actions and field observations should support each other. A normal screen value does not rule out a local leak, plugged line, or failed indication. When information conflicts, follow the plant’s verification and escalation procedure. Production pressure is not a reason to bypass an alarm or conceal uncertainty.
Ask how new operators qualify
Request the training progression for each unit or console. Find out how written knowledge, field demonstrations, emergency drills, and supervised shifts are evaluated. Ask about rotating shifts, overtime, respirator requirements, process-safety training, and the employer’s policy on fatigue. A credible trainee program makes authority limits clear before a new operator is left alone.
Sampling is another place where discipline matters. Confirm the correct point, purge or flush requirements, container, timing, and protective equipment before collecting material. Label it immediately and record the process condition, because a laboratory result without operating context may be misleading. If the sample cannot be taken as written, stop and ask. An improvised sample from the wrong line can expose the worker and send operations staff toward the wrong diagnosis.
Read the emergency procedures during training and locate the alarms, eyewash stations, showers, exits, muster points, and communication equipment in the field. Knowing their names on a quiz is not the same as finding them under pressure.
Sources
- U.S. Bureau of Labor Statistics: Data for Occupations Not Covered in Detail
- OSHA: Process Safety Management
Reviewed September 3, 2026: Chemical plant operator work depends on the process, equipment, shift pattern, safety procedures, and level of control-room responsibility. Ask local employers what entry-level operators handle before paying for training. Compare it with process technician work.